The second order is where a custom flatware programme is either confirmed or quietly derailed. The first order is visible and closely watched — the repeat arrives months later, produced from dies that have been used for other work, packed by a different shift and compared against whatever reference sample happens to survive in an office. This article sets out how a custom pattern is kept identical from the approved sample through repeat production, what has to be frozen, and what a buyer should be able to retrieve when a shipment is questioned.
In this article
- Why consistency is decided after approval, not before
- The freeze points that define a version
- The records that make a repeat a repeat
- What can still change, and what it costs
- Silent drift: the differences nobody agreed to
- Verifying that bulk matches the approved version
- Keeping a multi-SKU programme in step
- Frequently asked questions
Why consistency is decided after approval, not before
During development, the reference for a flatware pattern is a conversation: a comment sheet, a photograph of a handle in the hand, an email confirming that the bowl depth is acceptable. That is a perfectly good way to develop a product and a completely inadequate way to repeat one — because a conversation has no version number and no custodian.
Approval is the moment the reference changes from a discussion to an object. From that point the questions that matter are retrieval questions, not design questions: which sample is the reference, which drawing revision it corresponds to, and who holds both. Buyers who cannot answer those three questions immediately are not unprotected because a supplier is careless. They are unprotected because nothing in the programme was ever made retrievable.
Practical framing: a repeat order should be placeable with a quantity and a delivery date alone. If it also needs a photograph of the old sample, the programme is missing a record rather than missing a supplier.
The freeze points that define a version
A custom flatware programme passes through several natural freeze points, and each one locks a different part of the product. Treating them as a sequence rather than as a single approval is what makes version control possible.
| Freeze point | What becomes fixed | What is still open afterwards |
|---|---|---|
| Pattern and piece list | The silhouette and the utensils in the range | Finish, marking and packing details |
| Tooling and first article | Formed geometry, gauge and the decoration on the handle | Polish grade and colour consistency |
| Sealed reference sample | The physical standard for fit, feel and finish | Marking method and packaging artwork |
| Pre-production sample | The product as it will actually be produced, with the final marking | Packing configuration and shipment logistics |
| Packing approval | Carton quantity, assortment and labelling | Nothing that affects the product |
The practical value of the table is that it tells a buyer when a change is cheap. A request to alter the handle contour after the first article is effectively a new tooling project — while the same request made before the pattern is frozen is a line in a drawing. Most disputes about change cost are really disputes about which row of this table a programme had reached when the instruction was given.
The records that make a repeat a repeat
A repeat order needs five retrievable items. All five are produced during the first order, and none can be reconstructed accurately afterwards.
- A sealed reference sample held by both parties. One copy kept by the buyer and one retained by the factory as the production reference, carrying the final marking and finish rather than development trims.
- A numbered specification. Pattern revision, gauge, piece list, finish and marking, with a version identifier so that a later instruction can point at a specific version rather than at a memory.
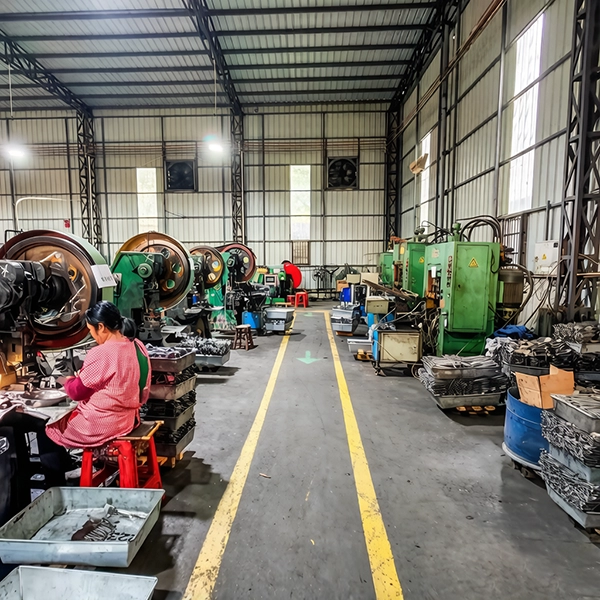
- The tooling record. Which dies exist, what they produce, who holds them and what condition they were in at the last run.
- The decoration and marking file. Artwork, engraving or stamping details and the placement used on the approved piece.
- The packing specification. Folding, count per carton, assortment and labelling, recorded as shipped rather than as briefed.
What can still change, and what it costs
Repeat orders are rarely exact repeats, and a programme that cannot accommodate change at all is a programme that gets replaced. The useful question is not whether a change is allowed but what it invalidates.
| Change on a repeat | Verdict | What it invalidates |
|---|---|---|
| Adding a colourway or a coated version | Routine | The finish approval only |
| More quantity, same specification | Routine | Nothing beyond material lead time |
| Changing the marking or logo method | Manageable | The sealed sample, which no longer describes the goods |
| Extending the piece list with serving items | Manageable | Nothing for existing pieces, but new tooling for new ones |
| Changing gauge or material | Costly | Forming behaviour, weight and often the dies themselves |
| Changing the handle pattern | A new programme | All of it, including the tooling |
The third row is the one most often overlooked. Once marking or packaging changes, the sealed sample no longer describes the order being produced, and holding one without noting the change is worse than holding none — because it looks like a reference without functioning as one. The remedy is procedural: when a repeat differs from the reference, the difference is written against the order and a new reference is sealed for the affected part.
Silent drift: the differences nobody agreed to
Most inconsistencies in repeat flatware are not defects — they are accumulated tolerances that each looked acceptable in isolation.
- Weight drift. Gauge varies within its own allowance, and handle forming takes up some of that variation, so a set can be a few grams per piece lighter than the original without any single piece failing a check.
- Finish drift. A polishing line changes abrasive or operator, and the same nominal finish reads slightly brighter or duller than the sealed sample.
- Marking drift. An engraving or stamping tool wears, so a logo that was crisp becomes shallower across a long run.
- Packing drift. Cartons are configured from the sizes available rather than the sizes specified, which is invisible until a retail customer opens them.
Drift is controlled by comparison, not by specification. A written tolerance says what is acceptable; an approved reference says what acceptable looked like on this programme. Both are needed — which is why the sealed sample and the numbering that connects it to a specific production run matter more than the wording of the tolerance band.
Verifying that bulk matches the approved version
Verification on a repeat order should be quick, because the specification has not changed, and it should still be deliberate. Four checks cover almost everything that goes wrong:
- Compare against the reference, not against memory. Put a production piece beside the retained sample on the same surface under the same light, and compare finish and marking before comparing measurements.
- Weigh a sample of pieces per item. Weight is the fastest single indicator that gauge and forming are still where they were, and it detects drift that visual inspection misses.
- Check the marking on a finished piece, not on a plan. Engraving depth and clarity are only visible on the goods.
- Confirm the packing configuration against the recorded specification. Assortment and carton quantity are part of the product for a retail programme.
Cheapest control point: a short pre-shipment check on the first cartons of a repeat costs very little and catches drift while the goods are still at the factory rather than at a port.
Keeping a multi-SKU programme in step
Once a range has more than one handle pattern or more than one finish, versions multiply and the risk of drift rises sharply. A programme with three patterns and two finishes has six product versions before any marking or packing variation is considered, and each combination carries its own reference sample.
| Programme size | Reference samples needed | Practical control |
|---|---|---|
| One pattern, one finish | One per party | A single numbered specification |
| One pattern, several finishes | One per finish | Shared pattern revision with finish-specific references |
| Several patterns, several finishes | One per combination | A version register recording which pattern revision sits with which finish |
The register is unglamorous — and it is the whole answer. A one-page record listing each SKU, its pattern revision, its finish reference, its marking version and the date it was sealed removes almost every retrieval problem a growing range creates, and it takes less time to maintain than a single disputed shipment takes to resolve.
Planning a repeating flatware range?
We produce custom flatware programmes from our Jieyang facility and keep sealed references and numbered specifications for every approved pattern, so a repeat can be placed against a version rather than against a photograph.
Frequently asked questions
How many reference samples should a programme keep?
At least two of the approved version: one held by the buyer and one retained by the factory as the production reference. Where an order will run across multiple shipments, the retained sample should be kept for the life of the tooling rather than for the life of the order, because that is the period over which the pattern is expected to stay identical.
Can I change the logo after the first order?
Usually yes, and it is one of the more manageable changes because it touches the marking rather than the formed geometry. What it does invalidate is the sealed sample, which no longer describes the goods being produced. The clean approach is to approve the new marking on a piece, seal a new reference for that version and record the change, rather than amending the order while leaving the old sample in place.
Why does a repeat order sometimes feel lighter than the first?
Because gauge varies within its own allowance and handle forming takes up part of that variation, so several pieces can end up slightly lighter without any individual piece failing a check. Weighing a small sample of pieces per item against the retained reference detects it quickly. The same logic explains small differences in finish brightness, which is why comparison against a retained sample matters more than any single written tolerance.
What should a repeat order reference?
A version, not a description. In practice that means the specification number, the pattern revision, the finish reference and the packing specification as shipped. An order that names those four can be produced without re-approval; an order that says only the same as last time depends on somebody still holding the same sample and the same file, which is a fragile arrangement for a programme intended to run for several seasons.
Do we need a new sample for every repeat?
Not when the specification is unchanged, which is the point of retaining a sealed reference. A pre-production sample is normally needed again when the piece list changes, when a new finish or marking is introduced, when the tooling has been re-cut, or after a long gap in production. For a straight repeat on the same version, comparing the first production pieces against the reference is faster and usually sufficient.
Consistency across repeat runs is not a by-product of good intentions. It comes from a numbered specification, a sealed reference held on both sides and a one-page register that says which version a piece belongs to. Everything else in a flatware programme can be renegotiated later — those three things only exist if they are created during the first order.