A flatware program rarely fails at the drawing stage. It fails later — at the first sample, at the transition from sample to tooling, or at the point where a pattern that looked perfect in a set of five has to be produced identically fifty thousand times. This article describes the development route we follow at Hongsheng Hardware from artwork to volume production, and the four points where the buyer's own decisions determine the outcome.
Stage 1 — Define the Pattern and the Piece List
Development starts with two documents, not one. The first is the pattern brief: silhouette, stem form, surface treatment, and the reference images or physical pieces the design is aiming at. The second is the piece list — exactly which items the set contains, and in what allocation. A 16-piece set, a 20-piece set and a 24-piece set of the same pattern are three different products, and the piece list must be fixed before tooling, because serving pieces often require their own forming tools even when they share the pattern language.
This is the first buyer decision point. Programs that lock the piece list early move quickly; programs that keep adding a gravy ladle or a cake server late in development pay for it in tooling time and schedule.
Stage 2 — Sample and Design Freeze
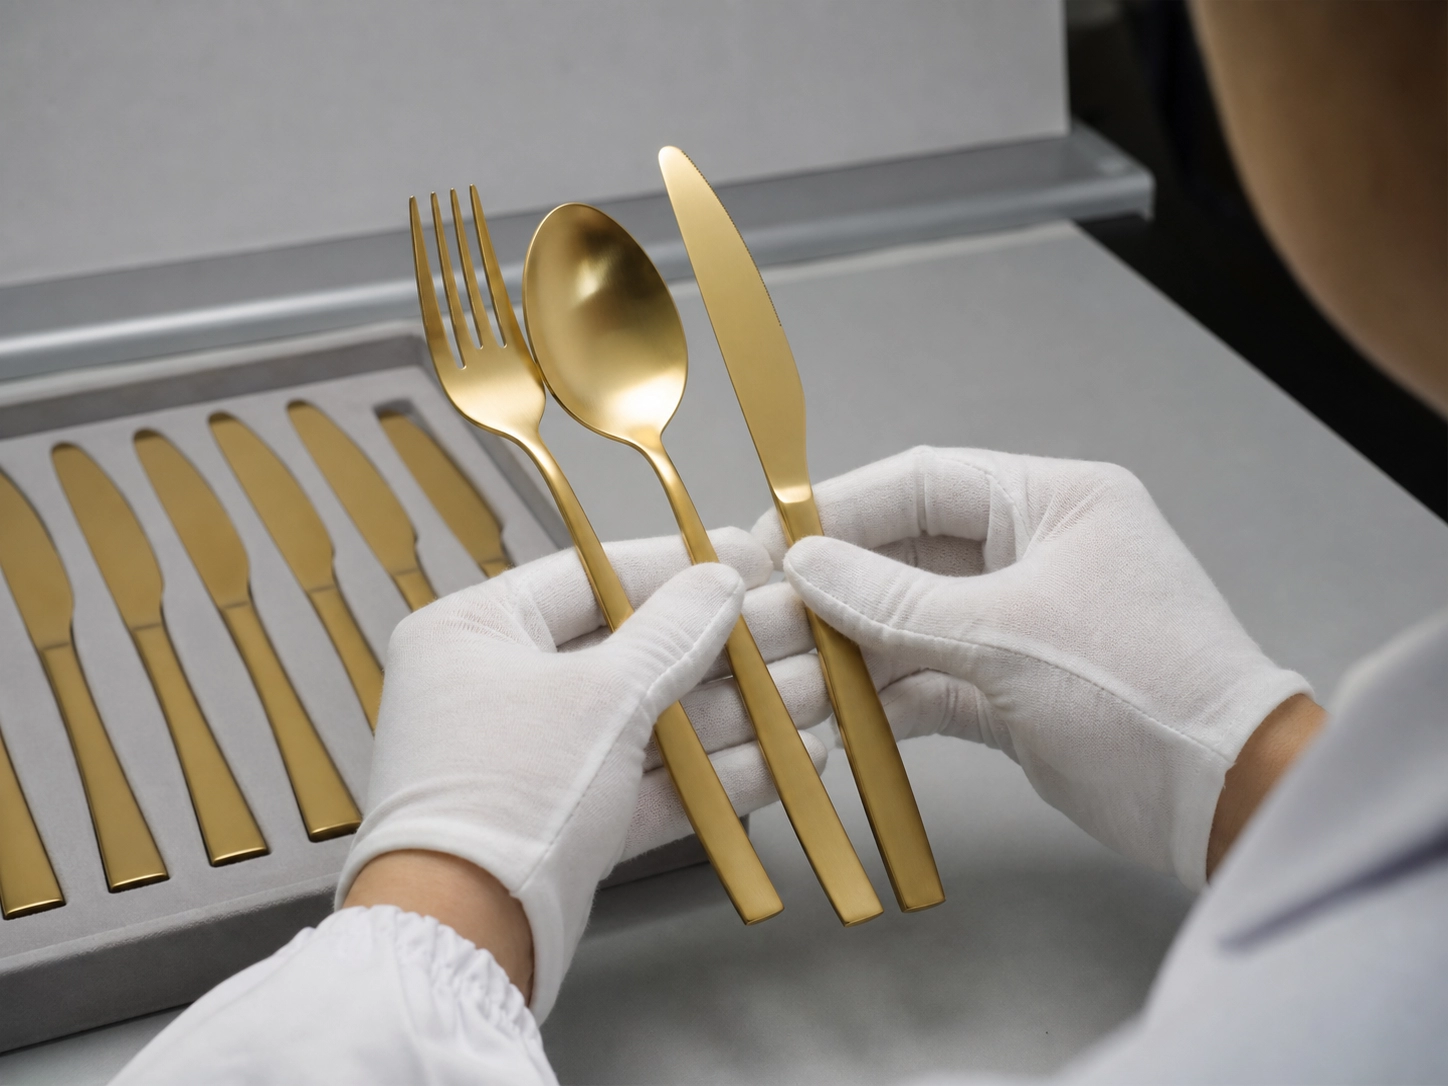
We produce samples for handling and visual approval before committing to production tooling. The sample stage exists to answer questions that a drawing cannot: does the stem sit correctly in the hand, does the embossed detail read at table distance, does the finish behave as intended across the whole surface rather than only on the show face.
The output of this stage is a signed sample and a frozen specification. From this point, the specification covers profile, edge break, finish and polish direction, piece weight, and the inspection basis. Anything not written down at this stage becomes a discussion at delivery instead of a decision at design. Our sample inspection checklist sets out how to run this approval properly.
Stage 3 — Tooling and First Article
With the design frozen, forming tools, trimming tools and any embossing or texturing tooling are produced. The first articles off the new tooling are measured against the frozen specification rather than against the sample alone, because a sample made with hand finishing can hide variation that tooling will expose.
| Control point | What is checked | Why it matters |
|---|---|---|
| Forming tool first article | Profile at defined stations, overall dimensions, symmetry | Establishes whether the tool matches the frozen drawing |
| Edge break | Sharps removed, radius consistent around the full perimeter | Safety and dishwasher durability both depend on it |
| Finish trial | Polish direction, scratch level, coating coverage | Finishing load is where schedule slippage usually originates |
| Weight and balance | Unit weight against specification, piece-to-piece spread | Weight variation is the fastest way for a premium set to feel cheap |
| Pattern repeatability | Detail alignment between items in the set | Side-by-side comparison on a laid table exposes any drift |
Stage 4 — Production, Incoming and Outgoing Control
Volume production is run against the frozen specification, with inspection at incoming material, in-process and before packing. Raw material is verified on receipt, because the single largest source of downstream failure in flatware is steel that does not behave as the specification assumes. Welded and hollow assemblies are checked at the seam, since a seam defect that survives polishing will fail in service.
This is the second buyer decision point: agreeing the inspection basis in advance. A buyer who states which defects are rejectable, and at what sample size, gets a clean shipment. A buyer who reviews appearance only at the port inherits every judgement call that was made on their behalf.
Stage 5 — Branding, Packaging and the Shipping Release
Branding and packaging are scheduled after the item specification is frozen, never in parallel with it. Logo execution changes the finishing sequence, and packaging changes the packing sequence, the carton count and the freight profile. Treating them as downstream steps keeps the metal specification stable and puts the branding decisions where they can still be changed cheaply.
- Logo execution. Engraved, etched, stamped or printed methods each interact differently with the surrounding finish and each needs its own approval sample.
- Transit protection. Individual wrapping, separation layers and carton arrangement are specified to protect visible metal surfaces, particularly on mirror and coated finishes.
- Marking and documentation. Carton marks, item codes and destination-market documentation are confirmed before the order is packed, so that the shipping release is a confirmation rather than a correction.
The third and fourth buyer decision points sit here: who owns the packaging brief, and who signs the shipping release. Programs that assign both clearly run to schedule; programs that leave the packaging brief to the factory receive a compliant box that does not fit the sales channel.
A Development Route You Can Plan Around
The route above is not unusual — it is simply written down. Its value is that each stage produces a document: a pattern brief, a piece list, a frozen specification, an inspection basis, a packaging brief and a shipping release. With those six documents, a flatware program can be quoted, scheduled and repeated. Without them, every reorder becomes a new negotiation.
Hongsheng Hardware has developed and manufactured Western tableware at our Jieyang base since 2008, integrating product development, production and sales, with the capacity to serve high-end hospitality pieces, classic household ranges and volume supply programs from one production system. Our Western tableware range shows the breadth of patterns currently in production, and our multi-piece set range illustrates how piece allocations are structured. To discuss a development program, contact us with your pattern reference and piece list.